How Do You Choose AI Tools for Automated Manufacturing Inspection?
TIME
Click count
A vision system may catch obvious scratches during a demonstration yet miss faint defects when parts rotate, lighting changes, or the line reaches full speed. It may also reject acceptable products so frequently that operators start bypassing it. Choose AI inspection tools by testing defect detection, false-reject rates, and complete inspection-cycle timing on representative production conditions—not by comparing headline accuracy alone.
Choosing AI tools for automated quality inspection manufacturing teams can trust starts with a clear inspection specification. Define what must be detected, which errors are tolerable, and how inspection decisions will reach the production equipment. Then compare suitable approaches through a controlled pilot, including integration work and ongoing maintenance in the purchase decision.
Define the inspection job before comparing software
“Find surface defects” is not a sufficient requirement. A scratch may be acceptable on a hidden face but unacceptable on a sealing surface. An assembly may look complete while containing the wrong component. Without explicit acceptance criteria, vendors can optimize demonstrations around different interpretations of quality.
Create a specification that connects visible evidence to a production decision:
- Defect definitions: Identify relevant defect types, locations, sizes, and severity levels. Include acceptable cosmetic variations that should not trigger rejection.
- Inspection conditions: Document part orientation, surface finish, conveyor speed, vibration, contamination, and available installation space.
- Decision requirements: Specify whether the system must classify a part, locate defects, measure dimensions, read markings, or verify assembly.
- Response requirements: Define the decision deadline, rejection mechanism, traceability record, and handling of uncertain results.
Separate visible-defect inspection from measurements requiring calibrated metrology. A model that highlights a suspected crack does not automatically provide a reliable crack-width measurement. Likewise, an optical system cannot establish internal integrity unless the sensing method reveals the relevant internal features.
Compare inspection approaches against the defects you actually have
The first comparison is not necessarily between vendors. It is between inspection methods. Conventional machine vision remains appropriate for stable geometry and clear rules; AI becomes useful where acceptable variation or defect appearance makes those rules difficult to maintain.
Consider a reflective machined component. A rule-based method might verify a hole position, while an AI model checks irregular surface damage. Combining them can be more practical than asking one model to handle every quality characteristic.
Anomaly detection deserves particular scrutiny when rejects are rare. Learning normal appearance can reduce dependence on defect labels, but “unusual” is not synonymous with “defective.” Test harmless changes in texture, supplier finish, and product markings alongside actual faults before accepting the approach.
Check image formation before judging the model
A software comparison is misleading if each candidate receives different-quality images. Motion blur, glare, inadequate resolution, and inconsistent triggering can hide defects before any algorithm sees them. A more sophisticated model cannot reliably recover evidence that the camera never captured.
Require an imaging feasibility check using representative parts. Confirm the smallest relevant defect is visible across the inspection area, including edges and difficult orientations. Assess exposure time at production speed, lens coverage, lighting stability, and whether several views or another sensor type are necessary.
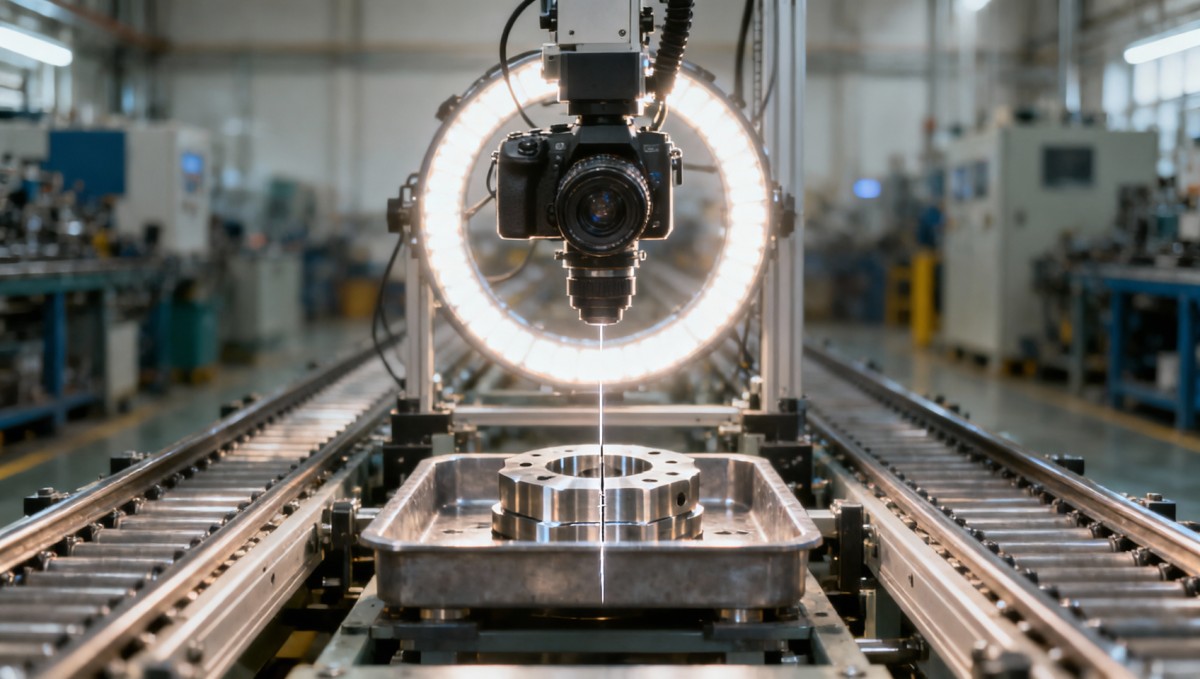
Lock the acquisition setup during comparative testing wherever practical. If a vendor proposes different optics or illumination, evaluate that as a complete system alternative and include its cost and installation constraints. Record those differences rather than attributing all performance gains to AI software.
Choose a delivery model your team can maintain
Software flexibility and operational ownership are separate purchasing decisions. A configurable platform may support many applications but still require substantial engineering. A packaged system can shorten deployment while limiting access to models, interfaces, or replacement hardware.
Packaged inspection systems
These can suit a defined station when internal vision expertise is limited. Compare the complete responsibility boundary: cameras, lighting, enclosure, commissioning, controls integration, and support. Ask which modifications require the supplier and whether adding a product variant changes licensing or service charges.
Configurable vision platforms
These offer reusable tools for teams operating several inspection stations. Evaluate how engineers label data, manage product recipes, review uncertain results, and deploy approved models. A polished training interface matters less if every line-side change requires specialist intervention.
Custom frameworks and development toolkits
Custom development can suit unusual sensors, demanding constraints, or an established internal machine-learning team. The trade-off is ownership of testing, deployment, cybersecurity, hardware compatibility, and future maintenance. Compare the full engineering workload with packaged options, not merely software license fees.
For any delivery model, clarify where inference runs. Edge processing can keep decisions local, but it still needs supported hardware and update procedures. Cloud services may support training or fleet management; determine whether production decisions depend on connectivity and what happens during an outage.
Run a pilot that exposes failure modes
Ask shortlisted suppliers to work against the same written acceptance criteria. A demonstration using selected images establishes feasibility, not production readiness. The pilot should test whether the system remains useful across normal variation and foreseeable disturbances.
- Build a representative dataset. Include product variants, shifts, material lots, tool wear, acceptable variation, and known defects. Retain borderline examples rather than removing difficult cases.
- Establish reference labels. Have qualified quality personnel resolve disagreements using the inspection specification. Record uncertainty when the reference decision itself is ambiguous.
- Separate development from evaluation. Keep final test data unavailable during tuning. Avoid placing near-identical images of the same part or acquisition sequence in both sets.
- Test on the line in shadow mode. Compare recommendations with established inspection decisions without immediately allowing the system to control rejection. Include startup, changeovers, and full-speed operation.
- Review errors and freeze the release. Examine misses and false rejects by defect type and operating condition. After tuning, validate the revised version on fresh holdout data before deployment.
Rare defects create an evidence problem. Repeated images of one damaged component do not establish performance across a defect category. Deliberately introduced faults can help test visibility and logic, but may not resemble naturally occurring defects. Document those limitations and retain an appropriate secondary control where evidence remains insufficient.
Use metrics that reflect production consequences
Overall accuracy can conceal poor defect detection when most parts are good. Require a confusion matrix and class-specific results. Define a miss rate as defective parts accepted divided by defective parts tested, and a false-reject rate as acceptable parts rejected divided by acceptable parts tested. Keep denominators explicit because supplier terminology can differ.
Evaluate critical defects separately from cosmetic ones. Also record uncertain decisions, manual-review volume, and performance by product variant. Report test sample counts with results; observing no misses in a small sample does not prove that the underlying miss rate is zero.
Compare candidates at operating thresholds that meet the same quality requirements. A system can appear more sensitive simply because it rejects more parts. The useful question is whether it can achieve the required detection level without creating an unacceptable sorting or rework burden.
Prove the decision reaches the correct part on time
Inference time is only one component of inspection latency. Image acquisition, preprocessing, transfer, decision logic, controller communication, and reject actuation all consume time. Test the complete path under sustained load, including bursts, multiple cameras, and competing hardware tasks.
Part tracking is equally important. A correct decision linked to the wrong conveyor position can create both escapes and unnecessary rejects. Verify trigger handling, encoder synchronization where relevant, result identifiers, and recovery after a stop or jam.
- Confirm compatibility with required PLC interfaces and MES or quality-system data exchanges.
- Specify behavior for missing images, low-confidence decisions, processing overruns, and communication failures.
- Check whether operators can identify the active product recipe, model version, and inspection status.
- Define image retention, access permissions, network boundaries, and permitted remote support.
Quality inspection must not be treated as a substitute for safety-rated machinery controls. Changes to reject mechanisms or equipment interlocks require review through the plant’s applicable controls and safety procedures.
Compare lifecycle cost and change ownership
The purchase price rarely captures the whole deployment. Request comparable quotations covering optics, lighting, industrial computing, fixtures, annotation, controls engineering, commissioning, operator training, and production time used for validation.
Then add recurring costs: licenses, support, storage, replacement hardware, model updates, and revalidation after process changes. Include the labor required to review false rejects and uncertain results. A low-cost tool can become expensive if it creates a permanent manual sorting task.
Use observed pilot results and plant-specific costs to compare expected operating impact. Keep assumptions visible, especially for rare escapes whose financial consequences may be uncertain. Do not convert a supplier’s accuracy claim directly into a savings estimate.
Before signing, establish who owns images and annotations, what can be exported, and whether inference continues if a subscription or support agreement ends. Ask how approved versions are backed up, restored, and rolled back. Model updates should have an approval path rather than appearing automatically on a production station.
Make acceptance criteria part of the purchase
Use mandatory gates before a weighted commercial comparison. A candidate that cannot reveal the target defect, meet the decision deadline, or satisfy required data controls should not win because it scores well on usability or price.
For candidates that pass, document the operating envelope: supported products, camera setup, line conditions, tested defect classes, decision thresholds, and maintenance responsibilities. Tie acceptance to repeatable tests at the installed station rather than a remote demonstration.
Finally, specify what triggers revalidation: a new material finish, relocated camera, changed lighting, revised product geometry, or updated model. Agree on who investigates rising rejects and who can authorize changes. These provisions turn a successful pilot into an inspection process the plant can keep under control.
Recommended News
- High-Throughput Production Systems: How Bottlenecks Affect OutputNov 08, 2026Discover how bottlenecks affect high throughput production systems and learn practical ways to improve flow, evaluate capacity, and increase good output.
- How Do You Choose AI Tools for Automated Manufacturing Inspection?Oct 27, 2026Compare AI tools for automated quality inspection manufacturing teams can trust. Learn to assess defect detection, false rejects, integration, and lifecycle costs before you invest.
- What Does Palletizing Mean? How Goods Are Stacked for Storage and ShippingOct 27, 2026What does palletizing mean? Learn how goods are stacked and secured for storage and shipping, explore key methods, and discover ways to improve load stability and reduce damage.
- High-Volume Distribution Centers: Comparing Automated Packing Costs and CapacityOct 27, 2026Compare automated packing solutions for high-volume distribution centers by throughput, total cost, and ROI. Discover how to cut cost per order and choose capacity that meets peak demand.
- Sizing an automation and power distribution system for future loadsOct 21, 2026Size your automation and power distribution system for future loads. Discover practical ways to forecast demand, scale controls, and plan expansion without costly oversizing.
All Categories
Hot Articles
- Audience Targeting for Regional Cultural Promotion: A Practical GuideNov 16, 2026Master regional cultural promotion audience targeting with practical tips to reach the right people, craft compelling messages, and drive participation.
- Oman Awards Two Duqm Green Hydrogen Projects and Opens Fourth Auction at COP31Nov 15, 2026Oman green hydrogen projects in Duqm target 121,000 tonnes annually by 2032. Explore the awards and a new auction linking hydrogen with green-powered data centers.
- Supplier Capability Metrics: How to Assess Capacity, Quality and DeliveryNov 15, 2026Use supplier capability metrics to assess capacity, quality and delivery. Learn how to verify claims, compare suppliers and reduce sourcing risks.